- Homepage
- About us
- Products
- Tapflo Solutions™
- Service
- Case Studies
- Resources
- Contact

In the Original Equipment Manufacturer (OEM) industry, fluid handling equipment is often a critical part of the overall machine design. As pumps must be integrated into larger assemblies and adapted to specific process requirements, ease of integration and flexibility are key selection criteria. Tapflo supports machine builders by providing expertise and engineered solutions that can be tailored to different industries, media characteristics and installation constraints.
By selecting the right pump for the application, our clients improve manufacturing equipment reliability and simplify maintenance. In addition to supporting standard machine development, Tapflo engineering team works on customized projects requiring dedicated configurations, integrated modules or application-specific modifications. This enables machinery manufacturers to create energy efficient designs and dependable devices while maximizing the return on investment.

We understand that every company has unique needs, which is why we offer personalized solutions tailored to specific requirements. Our team of engineers is always ready to advise and help you choose the best solution.
Tapflo Solutions is a department created in response to the demanding and unusual needs of the market, going beyond the scope of our standard offer. We specialize in designing unconventional solutions that meet the most difficult customer requirements.
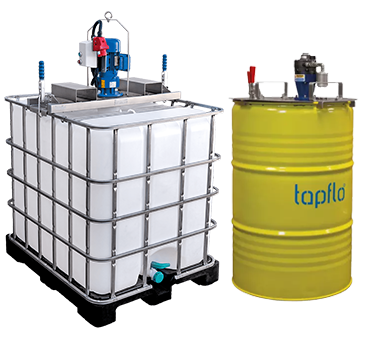
Devices created by SolutionsTM are comprehensive solutions that increase work comfort and safety, such as stationary and mobile systems for unloading media from tanks, drums or IBC containers, mixers and mixing stations or systems for the production of SLES.
We also add functional modifications to standard devices from the Tapflo portfolio, e.g. by increasing their mobility, adjusting dimensions or introducing advanced safety and control systems.
We also offer a wide range of products designed to protect Tapflo equipment from damage or weather conditions – such as thermal or acoustic covers.

Proper maintenance of pumps is critical to ensuring reliable and uninterrupted operation in any industry. Using only original Tapflo spare parts guarantees that every component meets strict quality standards, ensuring optimal performance and longevity of your equipment.
In demanding environments, including chemical processing and ATEX zones, genuine parts help prevent unexpected breakdowns, minimize costly downtime, and maintain the safety and efficiency of your operations.
Investing in original Tapflo components provides businesses with peace of mind, enabling continuous production and long-term reliability for all pumping systems.

Many OEM-designed modules require reliable handling of fluids used in production, cleaning and utility operations. The transfer of acids and alkalis, detergents, aggressive chemical solutions and other process chemicals are examples of applications found in industrial manufacturing facilities. Pumping equipment is also commonly integrated into systems for filling and emptying chemical storage tanks, automated batch transfer stations and solvent handling units operating in hazardous areas. Depending on the requirements, these solutions may also be designed for energy-efficient chemical transfer, continuous process liquid circulation and safe operation with potentially corrosive media through the use of appropriately selected pump materials, including corrosion-resistant metals and engineered plastics.

Automated process systems often rely on the controlled transfer of chemicals and additives between storage, preparation and use stages. Typical applications include the transport of flocculants, coagulants and other process media, as well as automated batch transfer procedures. Tapflo industrial pumps can be integrated into dosing skids, chemical preparation units, sterile packaging systems and process control systems, where reliable fluid transfer, precision flow control and compatibility with automation equipment are essential for stable production conditions.

Fluid handling equipment is widely used in auxiliary systems supporting industrial machinery and production processes. Common applications include the transfer of coolants and lubricants in CNC machines, pumping of machining fluids and circulation of cooling media in welding process cooling systems. Industrial pumps are also incorporated into process liquid circulation loops and other utility circuits where reliable continuous operation is required to maintain stable performance, temperature control and equipment protection.

Machine builders supplying equipment to the food and beverage, cosmetics and pharmaceutical sectors often require hygienic fluid handling solutions suitable for sensitive products and cleaning procedures. Typical applications of Tapflo's pumps include the transfer of liquid and semi-liquid food ingredients such as dairy products, syrups, concentrates, sauces, fruit purees, chocolate and confectionery products, as well as creams, lotions and other personal care formulations. Fluid handling equipment may also be integrated into CIP systems used for cleaning process installations and maintaining hygienic operating conditions while supporting consistent product quality.

Many industrial processes involve products with challenging rheological properties or specific handling requirements. Pumps and mixers are commonly used for the transfer of paints, coatings and varnishes, pumping of adhesives and sealants, circulation of inks in printing equipment and transfer of pigment slurries. OEM equipment can also incorporate mixing stations for paint and varnish emulsions in IBC containers, helping maintain product homogeneity and consistent quality prior to transfer or further production stages.

Wastewater treatment applications represent an important area for OEM fluid handling systems. Typical examples include industrial wastewater neutralisation, filter press feeding and sludge transfer. Pumps are also used for handling contaminated water, lime milk and water suspensions containing dissolved or suspended solids used in industrial water infrastructure projects. Depending on the installation, additional protection devices can be incorporated to prevent dry running and overpressure conditions, helping reduce downtime and service costs.

Container unloading and bulk liquid transfer are among the most common applications in equipment for original equipment manufacturers. Industrial pumps and mixers can be integrated into drum and IBC unloading systems, stations for emptying barrels with process liquids and tank filling and emptying units. Additional applications include tank-to-tank transfer, mobile pump skids and automated fluid transfer stations designed for handling chemicals, cleaning agents and other industrial liquids.

OEM solutions often need to transfer media that cannot be handled efficiently by conventional pump configurations. Typical examples include transfer of solids-laden and high-viscosity media, as well as pumping of shear-sensitive products where preserving product properties is important. Selecting the right pump technology and construction allows stable handling of demanding media. In many cases, high-performance pumps are required to handle abrasive slurries, viscous chemicals and fluids containing solids to maintain reliable performance in demanding production environments.